
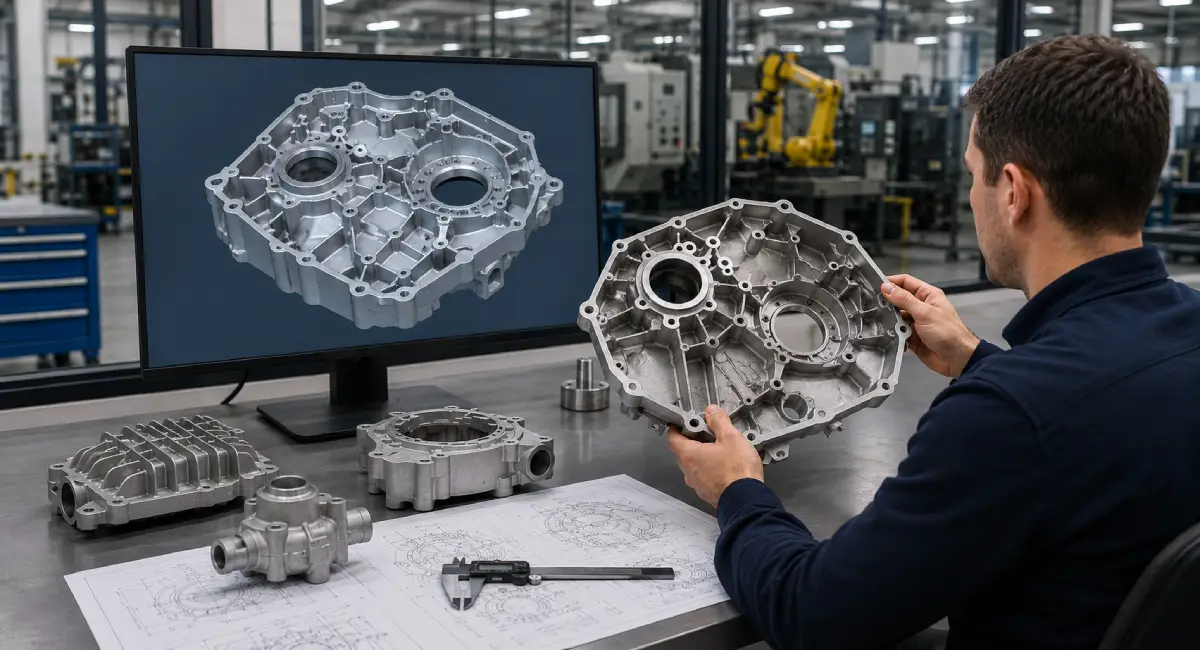
Aluminum castings can look perfect on the outside and still be hiding a problem deep inside. A pore the size of a pinhead, a pocket of shrinkage tucked in a thick section, a bit of foreign material trapped in the metal. None of it shows on the surface, and all of it can compromise a part that has to hold pressure, carry load, or survive vibration. That is the problem radiographic testing exists to solve. It lets inspectors see inside a finished casting without cutting it open, using X-rays to reveal internal defects before the part ever leaves the foundry.
If you buy castings, machine castings, or design products around them, understanding how this inspection method works will make your sourcing conversations a lot more productive. This guide explains the process in plain language: what it is, what it finds, when you need it, and what to ask for.
The Basic Idea: Seeing Through Metal
The principle behind radiographic testing is simple. X-rays pass through material, but they do not pass through evenly. Dense, solid metal absorbs more radiation, while voids, gas pockets, and less dense inclusions absorb less. When the radiation that makes it through the part strikes a detector on the other side, it creates an image of the part’s internal structure, much like a medical X-ray shows bone through skin.
On the resulting radiograph, internal defects show up as dark spots or irregular shapes against the lighter background of sound metal. A trained inspector reads that image and evaluates what is there: whether the indications are within acceptable limits for the application, or whether the part should be rejected.
The key word in all of this is nondestructive. The part is examined, evaluated, and returned to the production stream intact. Nothing gets cut, sectioned, or sacrificed. That matters enormously for expensive components, because a destructive test tells you about the one part you destroyed, while a nondestructive test tells you about the part you are actually shipping.
What Radiography Actually Finds
Castings are produced by pouring molten aluminum into a mold, and the physics of that pour creates the potential for specific internal flaws. Radiography is well suited to catching the volumetric defects that casting processes can produce:
Porosity refers to small gas pockets trapped in the metal as it solidifies. A few scattered pores may be harmless in a low-stress part, but porosity in a pressure housing or a load path is a real problem.
Shrinkage happens because metal contracts as it cools. In thick sections or spots where the metal cools last, that contraction can leave sponge-like voids. Shrinkage is one of the most common and most serious casting defects, and it hides exactly where stress tends to concentrate.
Voids and cavities are larger empty spaces, often caused by poor feeding during solidification or turbulence in the pour.
Inclusions are foreign material, such as pieces of the mold, slag, or oxide films, that got trapped in the metal. They create weak spots and can act as crack starters under cyclic loading.
What radiography is less suited to finding is tight cracks, especially ones oriented in certain directions relative to the X-ray beam. That is a job for other methods, most notably ultrasonic testing, which uses high-frequency sound waves instead of radiation. The two methods are complementary: radiography gives you a picture of volumetric defects across the whole part, while ultrasonic testing is strong at finding planar flaws like cracks in solid sections. For complex castings with irregular geometry, radiography is usually the more practical choice, which is why it remains the workhorse inspection method in foundries.
When a Casting Actually Needs It
Not every part needs to be X-rayed, and insisting on it for everything just adds cost. Radiographic inspection earns its price on parts where an internal defect could cause a failure that matters. Typical candidates include:
- Components with load-bearing requirements, where an internal void could initiate a crack
- Pressure-containing parts like pump and valve housings, where porosity means leaks
- Parts with thick sections or complex internal geometry, where shrinkage risk is highest
- Applications involving sustained vibration or fatigue loading
- Parts built to military or OEM specifications that explicitly require radiographic inspection
A good rule of thumb: if the drawing or contract calls it a critical characteristic, radiography is probably on the table. If the part is a simple bracket in a benign application, it probably is not worth the cost.
Where the Inspection Fits in the Process
The most valuable placement of radiography is before expensive downstream operations. Consider the economics. A casting might receive several machining operations, surface finishing, assembly into a larger unit, and then testing before an internal defect is discovered. Every one of those steps adds value to a part that was already doomed. Catching the defect at the foundry, before machining, means scrapping a cheap casting instead of an expensive finished component.
This is why foundries that offer in-house radiography integrate it into the production plan rather than treating it as an afterthought. The inspection becomes a gate: only castings that pass advance to the next stage. For the customer, that translates into fewer surprises downstream and a much more predictable supply of good parts.
What You Get From an Inspection
A radiographic inspection is not just a pass or fail verdict. It produces documentation. The radiograph itself is a permanent record of the part’s internal condition, and it typically comes with a written report describing what was found and how it was evaluated against the applicable acceptance criteria.
That record has real value. If a question ever arises about a part’s quality, years after shipment, the radiograph can be pulled and reviewed. For industries with audit requirements, defense work, or long warranty obligations, that traceability is often a contractual requirement rather than a nice-to-have.
A Few Practical Notes for Buyers
If you are sourcing castings and want radiographic inspection, a few points will make the process smoother.
First, specify the requirement early. Radiography is not something most foundries apply by default, and it needs to be called out on the request for quote and the purchase order, along with the applicable specification or acceptance standard. Vague instructions lead to disputes later.
Second, understand that inspection criteria vary. The same radiograph can be acceptable under one specification and rejectable under another. Make sure you and your supplier are working from the same standard, and that the standard matches the part’s actual service conditions.
Third, ask how results are delivered. You should expect the images, a written evaluation, and a summary you can file with your quality records.
Finally, remember that radiography is a verification tool, not a substitute for good process control. The best foundries use solidification simulation and careful gating design to prevent defects from forming in the first place, then use radiography to confirm the result. When you evaluate suppliers, the ones who talk about both prevention and verification are the ones who have their quality story in the right order.
The Bottom Line
Radiographic testing takes the guesswork out of the question every casting buyer faces: what is inside this part? It is a mature, well-understood method that catches the internal defects visual inspection cannot, protects downstream operations from wasted work, and creates a documented record of quality that follows the part for its entire life. For critical aluminum castings, it is one of the least expensive forms of insurance available, and knowing how to specify it correctly is a genuinely useful skill for anyone who sources cast components.